The bigger the pour in crude casting process the more splatter or run off out of the "gate".
Pouring a little too much and having it run out is much better than not enough and a void resulting.
The "ladle" or whatever holds the molten material can be dumped out too.
While it could be reheated in the ladle , it is not desired,usually . Depends on how it is heated ,ladle and furnace or heat source design ...ect..
Too if slag or impurities are present in the dregs ,just dump them. A poor fit of mold halves , or a vent to conduct flow of material into more complicated designs and allowing gas to escape too would have some "run out"..
Before making a pour , impurities can be inspired to rise to the top with a flux.
Then a "slagger" (a type of crude skimmer of which I have replaced the angle iron ends of very many in an iron works ) can skim the majority off the top of the molten material.
To clean a ladle of hardened or accumulated slag it must be empty too.
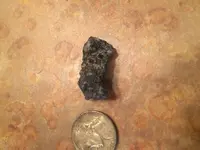
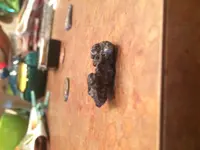
Your finding may be a splatter made during casting when a gate is overfilled. An air bubble could cause a pop..a vent in the mold cavity to conduct flow could ooze material ,a poor fit of mold halves ect... ...
Sand with a binding agent or two can be used to hold the shape of the removed pattern.
Excess material poured on it would be flat or shaped to the sand it landed on , contaminated on one side more than the other , and more rounded on the surface side.
Many impurities throughout might suggest material pulled off with a slagger and allowed to hit the ground/floor.